TEST REPORT · XLH-TEST-001
CO₂ Laser Production Test of POM Embosser Dies
This report documents one real XLH Laser production example in which the DF60D 60W CO₂ laser was used to engrave and cut a matched male and female POM embosser die set, followed by separate assembly and physical embossing verification.
TEST CONDITIONS
Core Production Data
The values below describe the documented production example shown in the test video. They are not universal production guarantees.
Actual processing time varies with artwork complexity, die dimensions, engraving area and production requirements.
CORE PRODUCTION TEST
Laser Engraving & Cutting Production Test
The production video documents one real DF60D processing cycle from positioned POM material through engraving and cutting of the matched die components.
The footage has been edited and accelerated for practical web viewing. The video runtime is not the production time. An independent timer remains visible in the recorded scene and shows 03:35 at completion.
The approximately 3 minute 35 second figure refers to laser engraving and cutting of the matched die set shown in this production example. It does not include later installation, pressing or application photography.
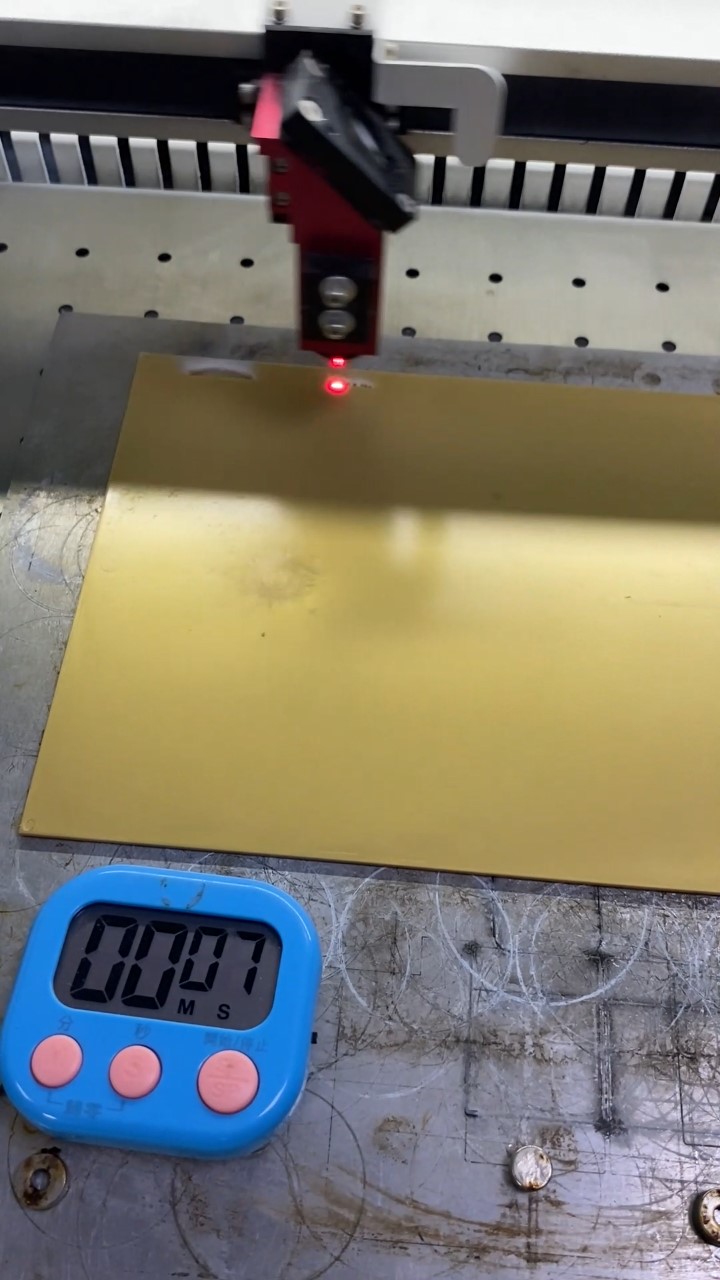
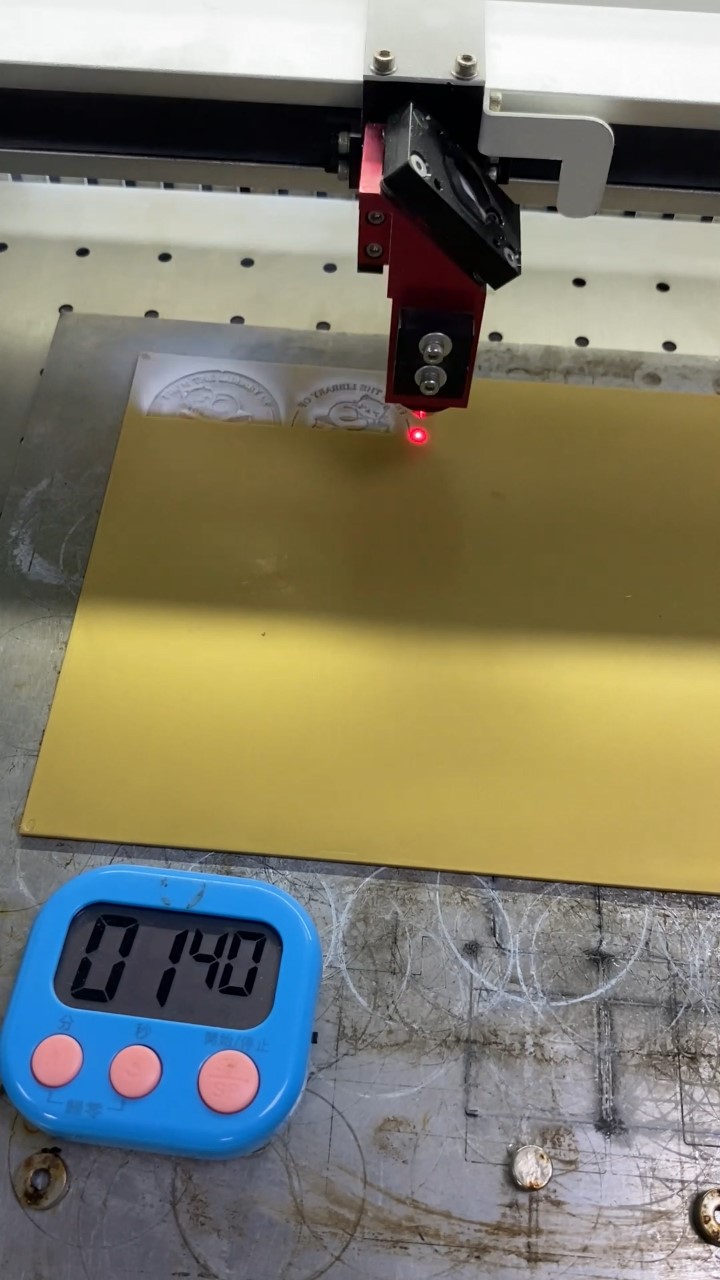
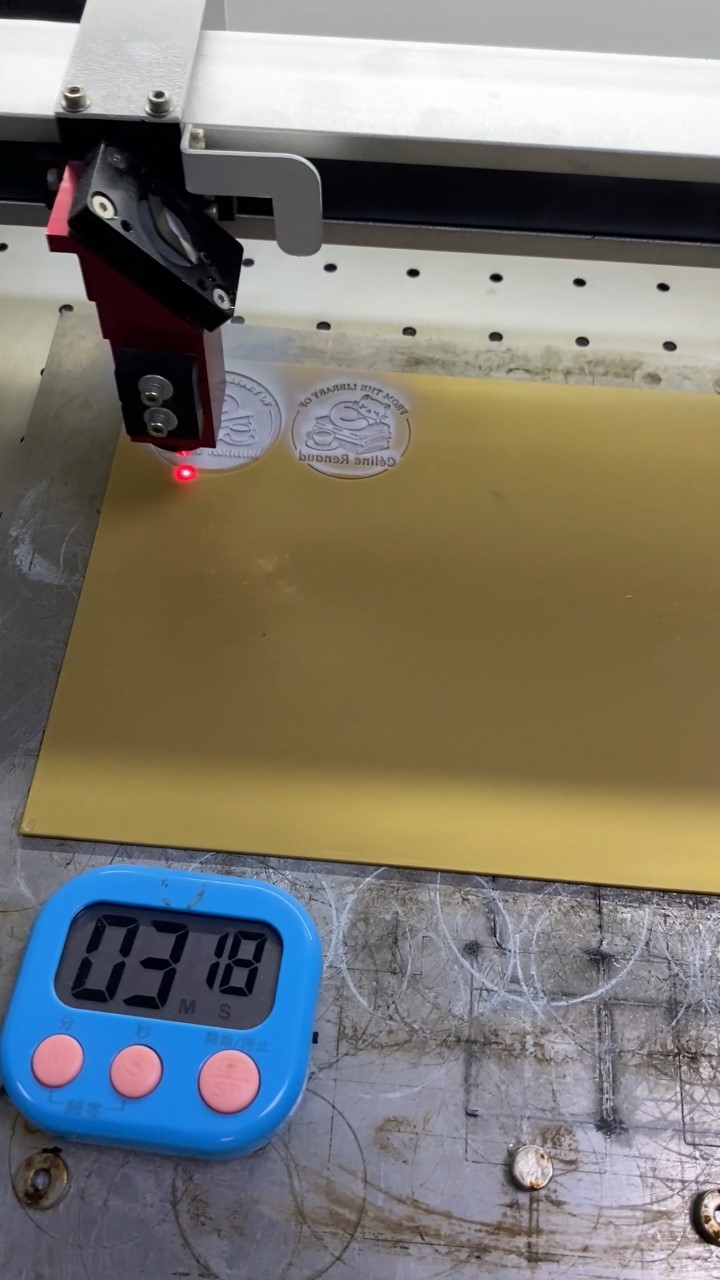
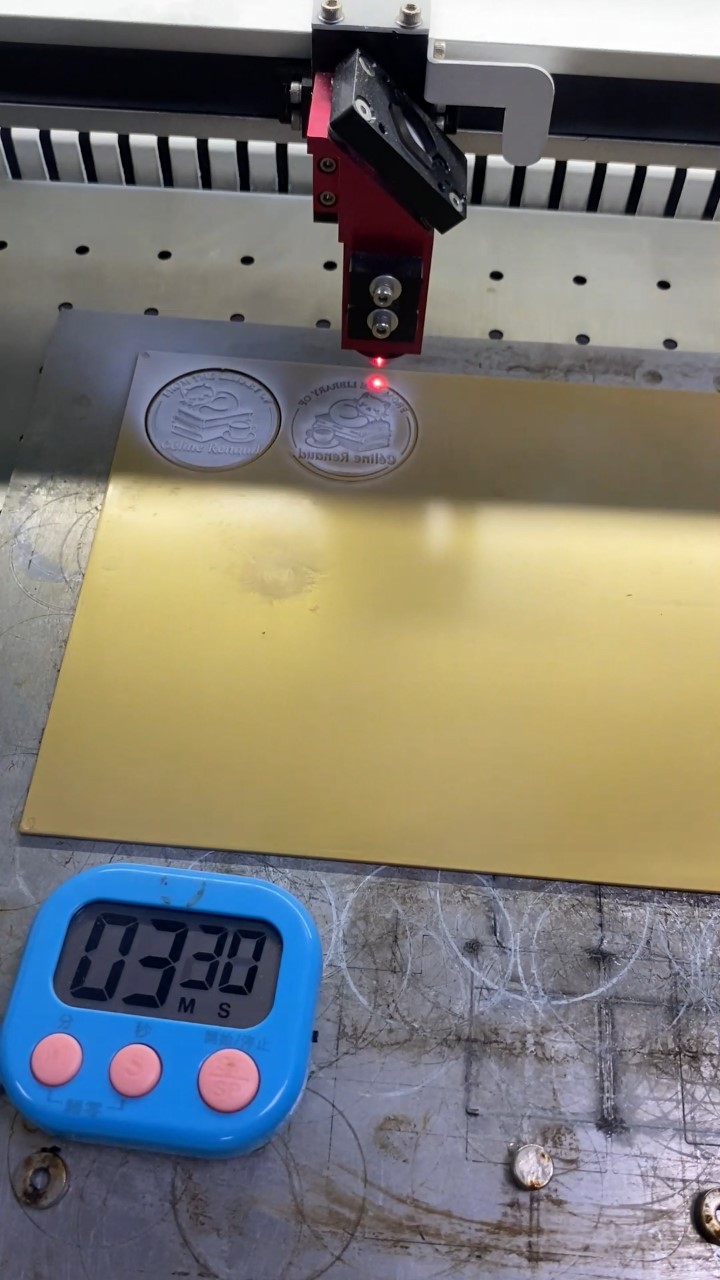
This observed timer reading supports the stated demonstrated processing time of approximately 3 minutes 35 seconds for the matched die set shown. Normal variation can occur according to the specific job.
ASSEMBLY & FUNCTIONAL VERIFICATION
Assembly & Functional Verification
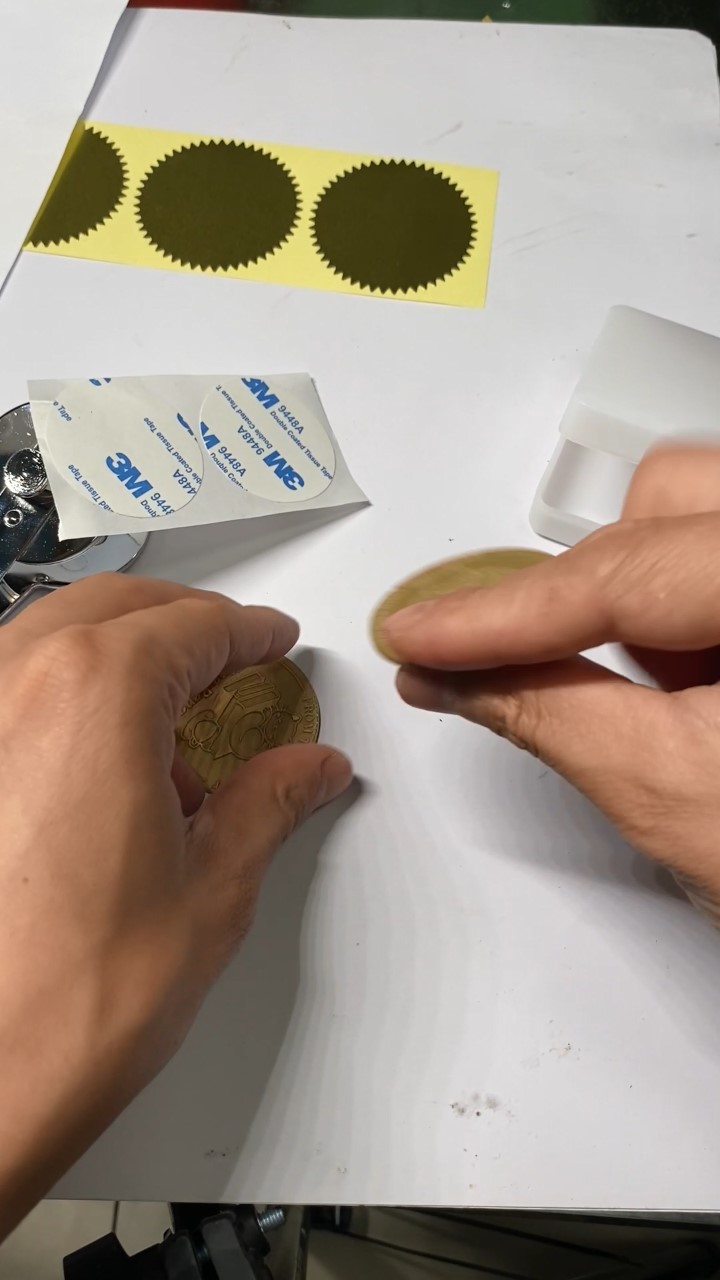
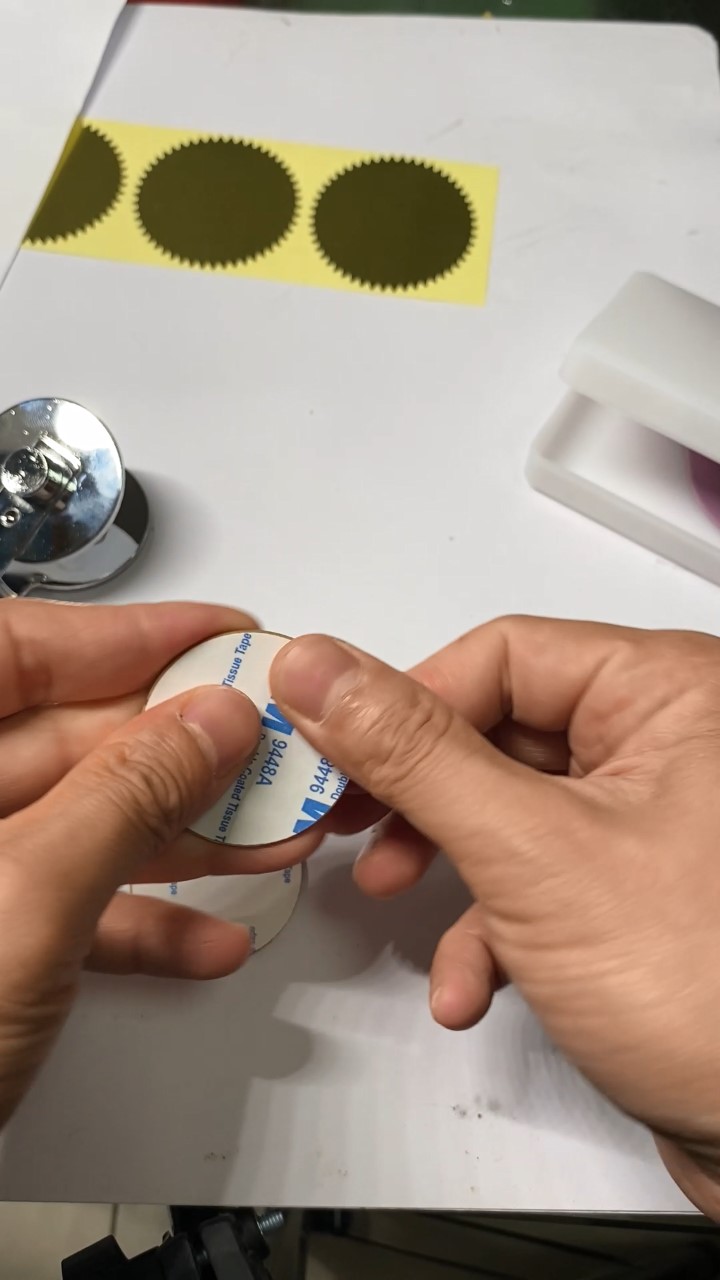
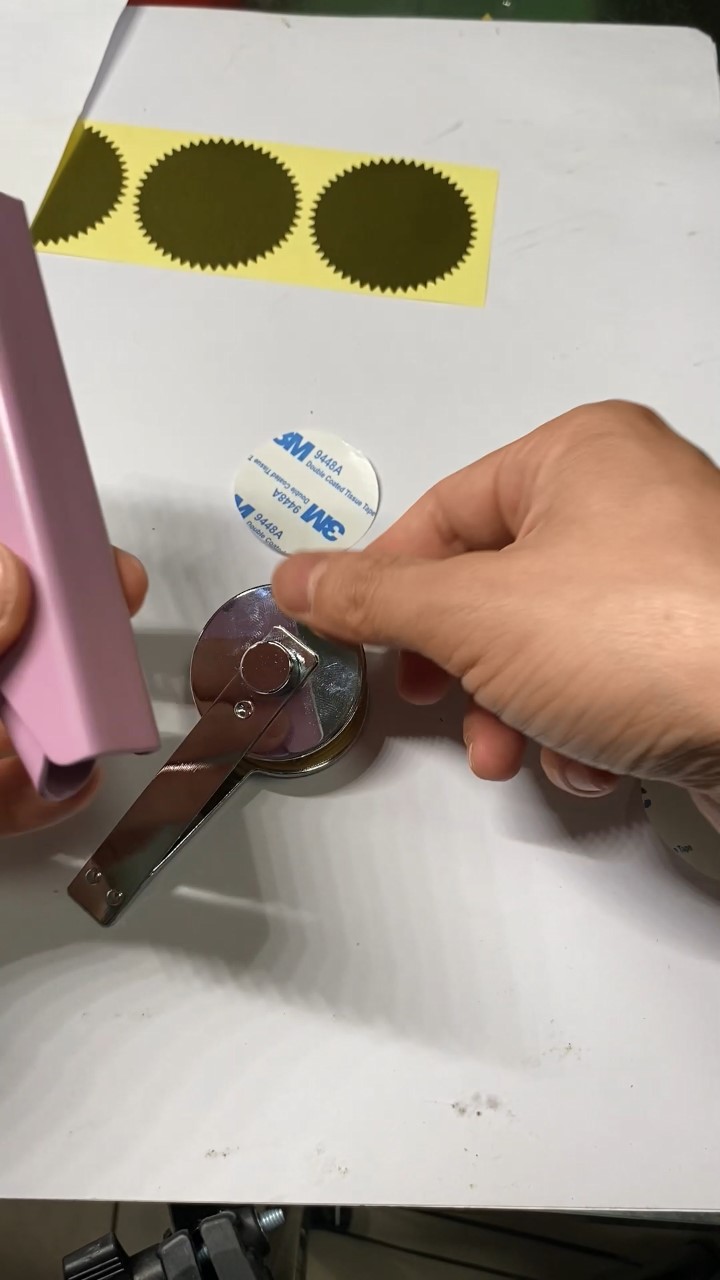
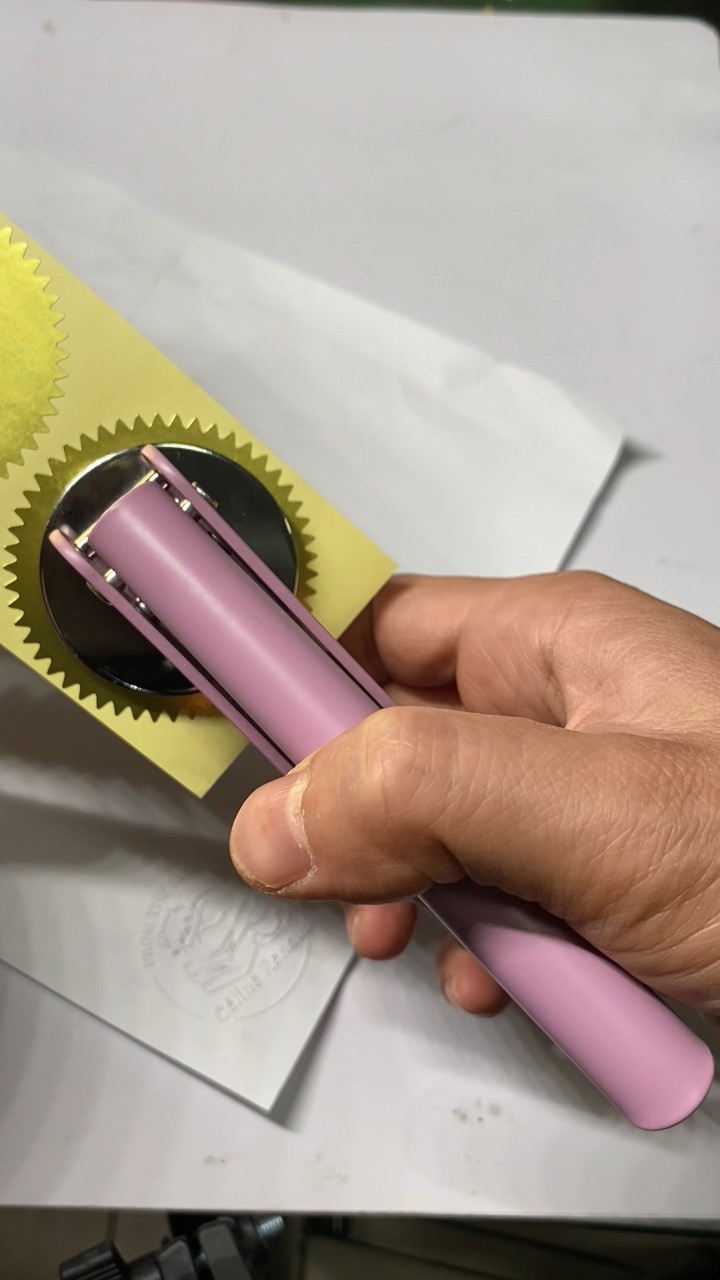
After laser processing, the finished POM die components are prepared, aligned and installed in a handheld embosser before an actual pressing check.
This second video demonstrates how a finished POM die set can move from die preparation to installation in working embosser hardware and actual pressing. This sequence is documented separately from the timed core production test and is not presented as the same timed specimen.
ADDITIONAL APPLICATION VERIFICATION EXAMPLES
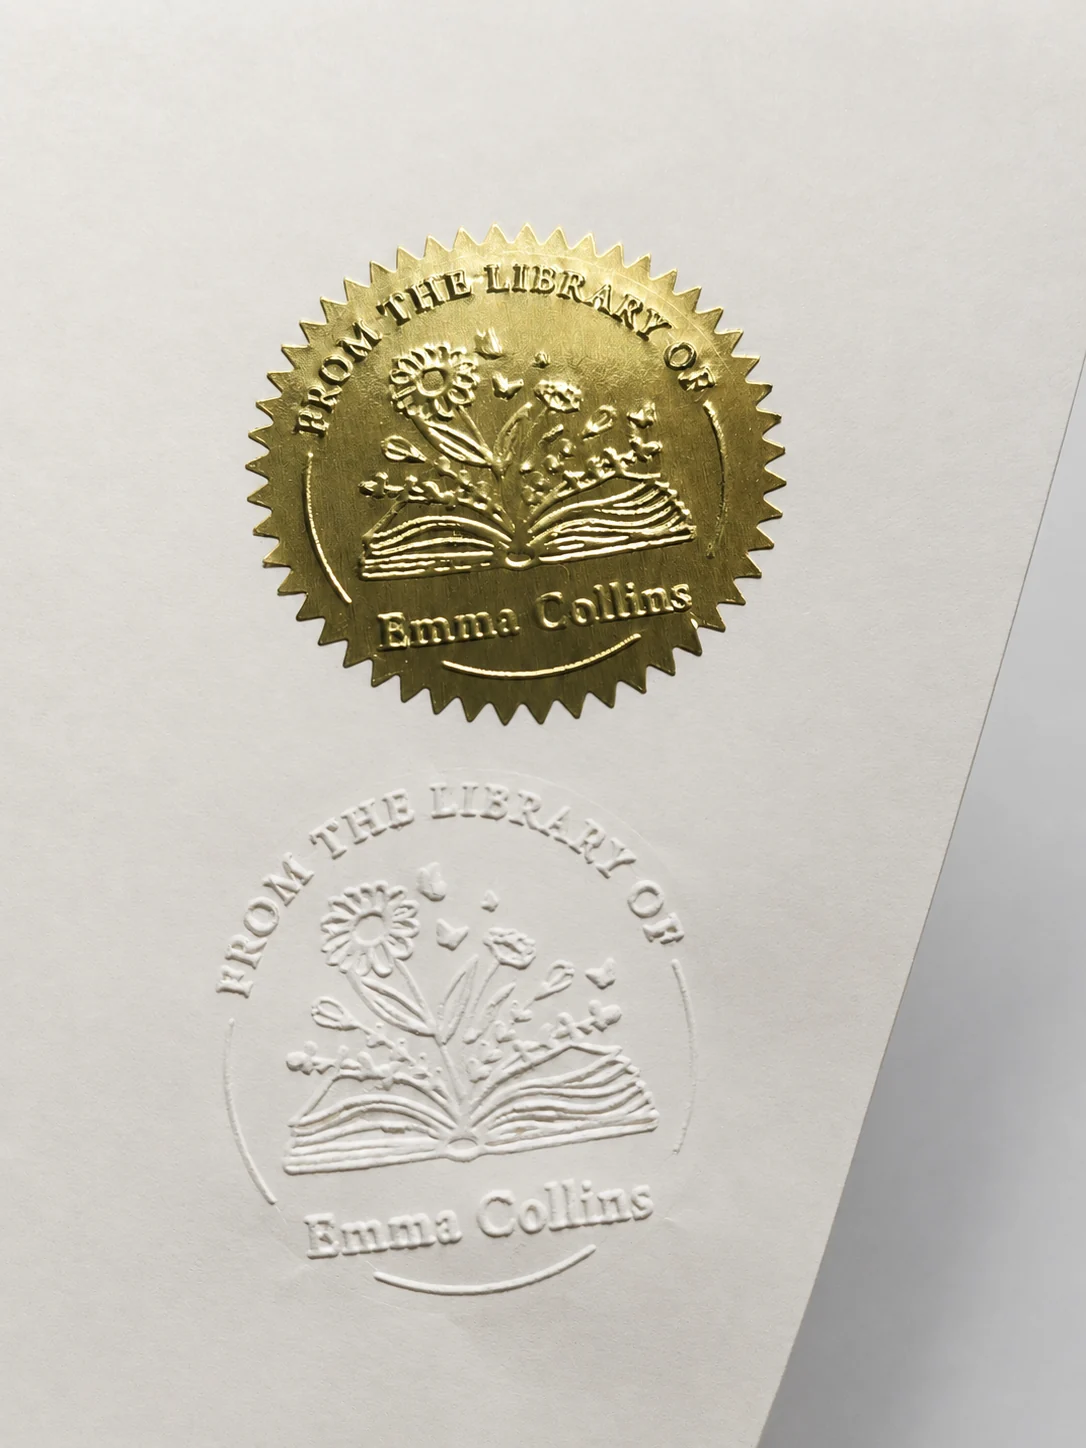
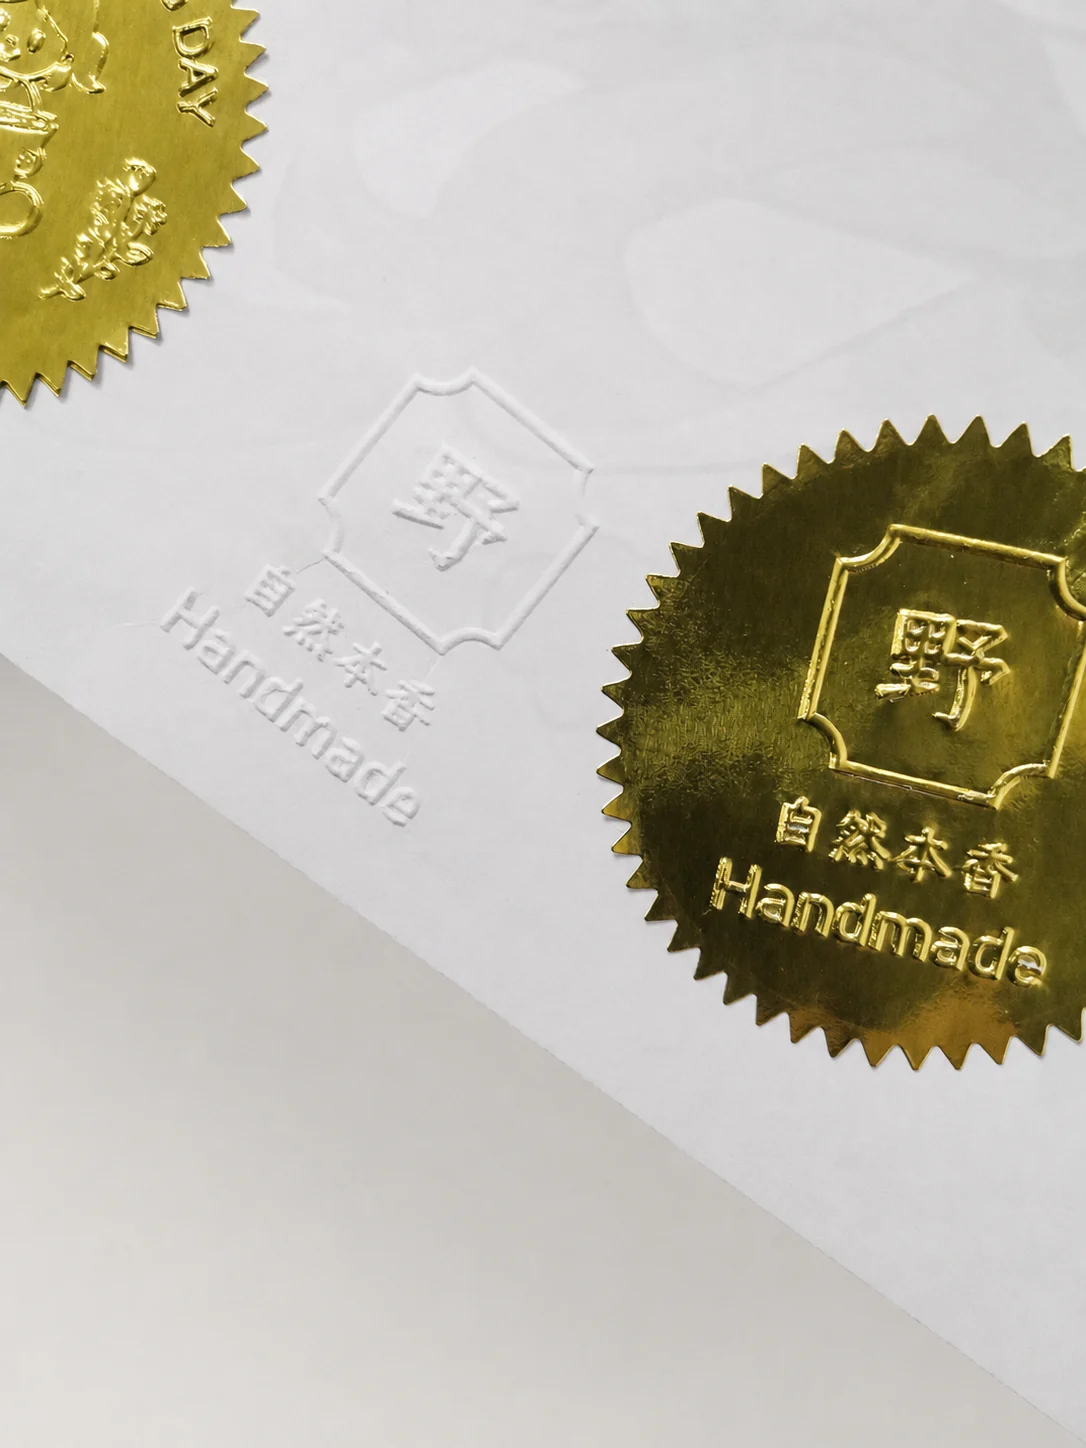
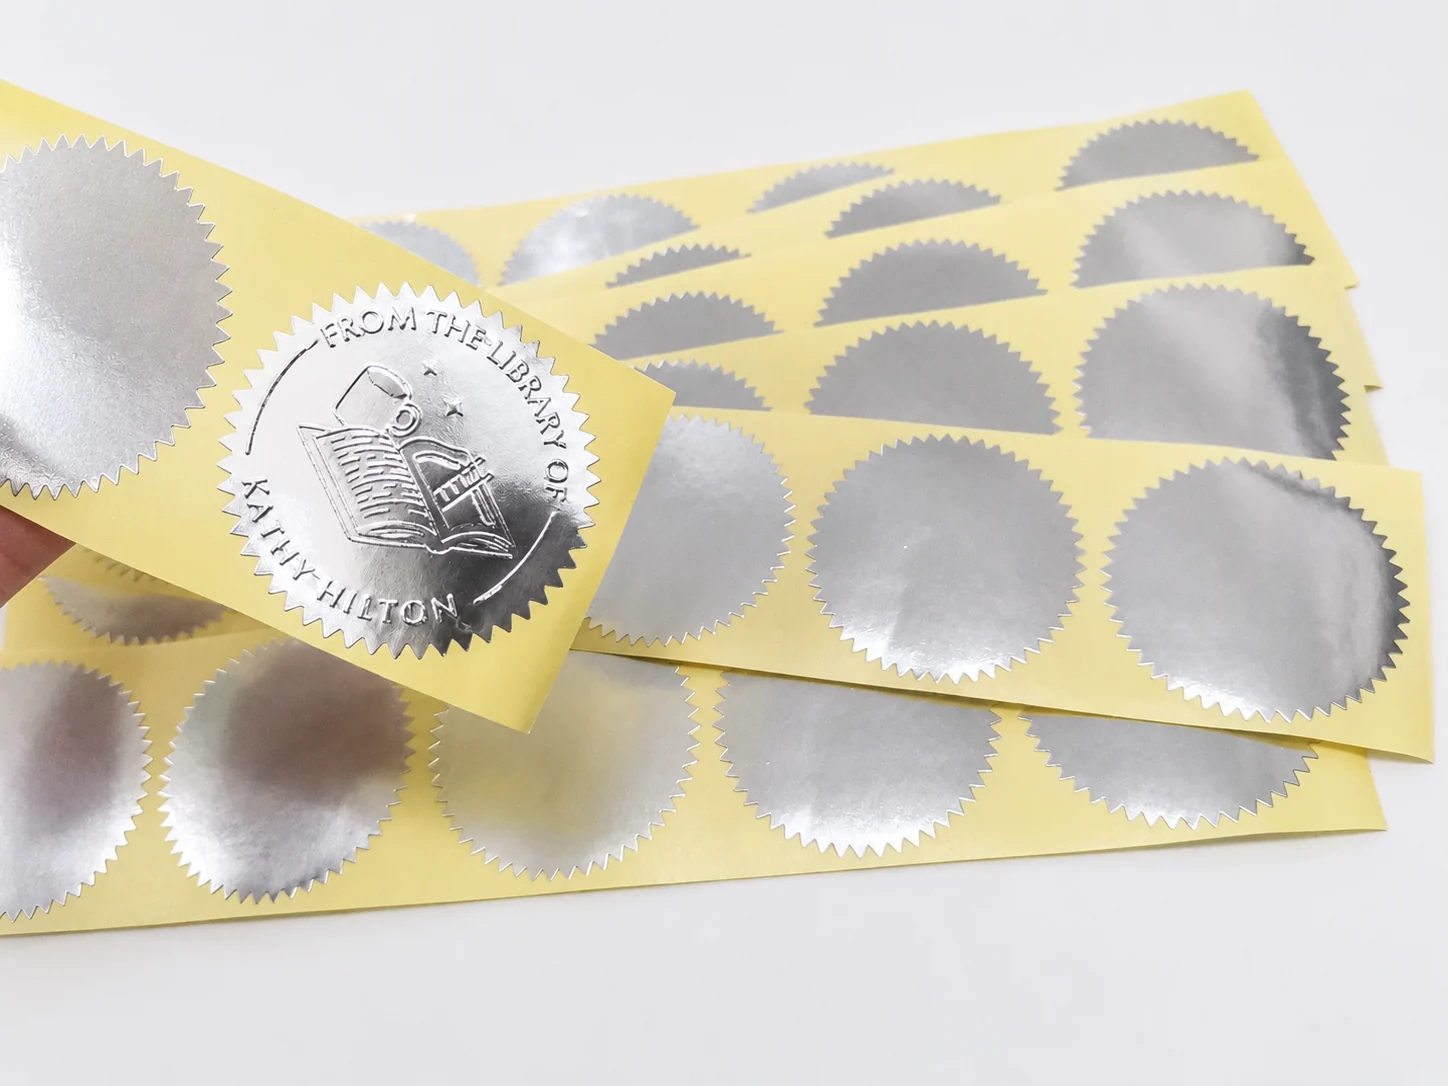
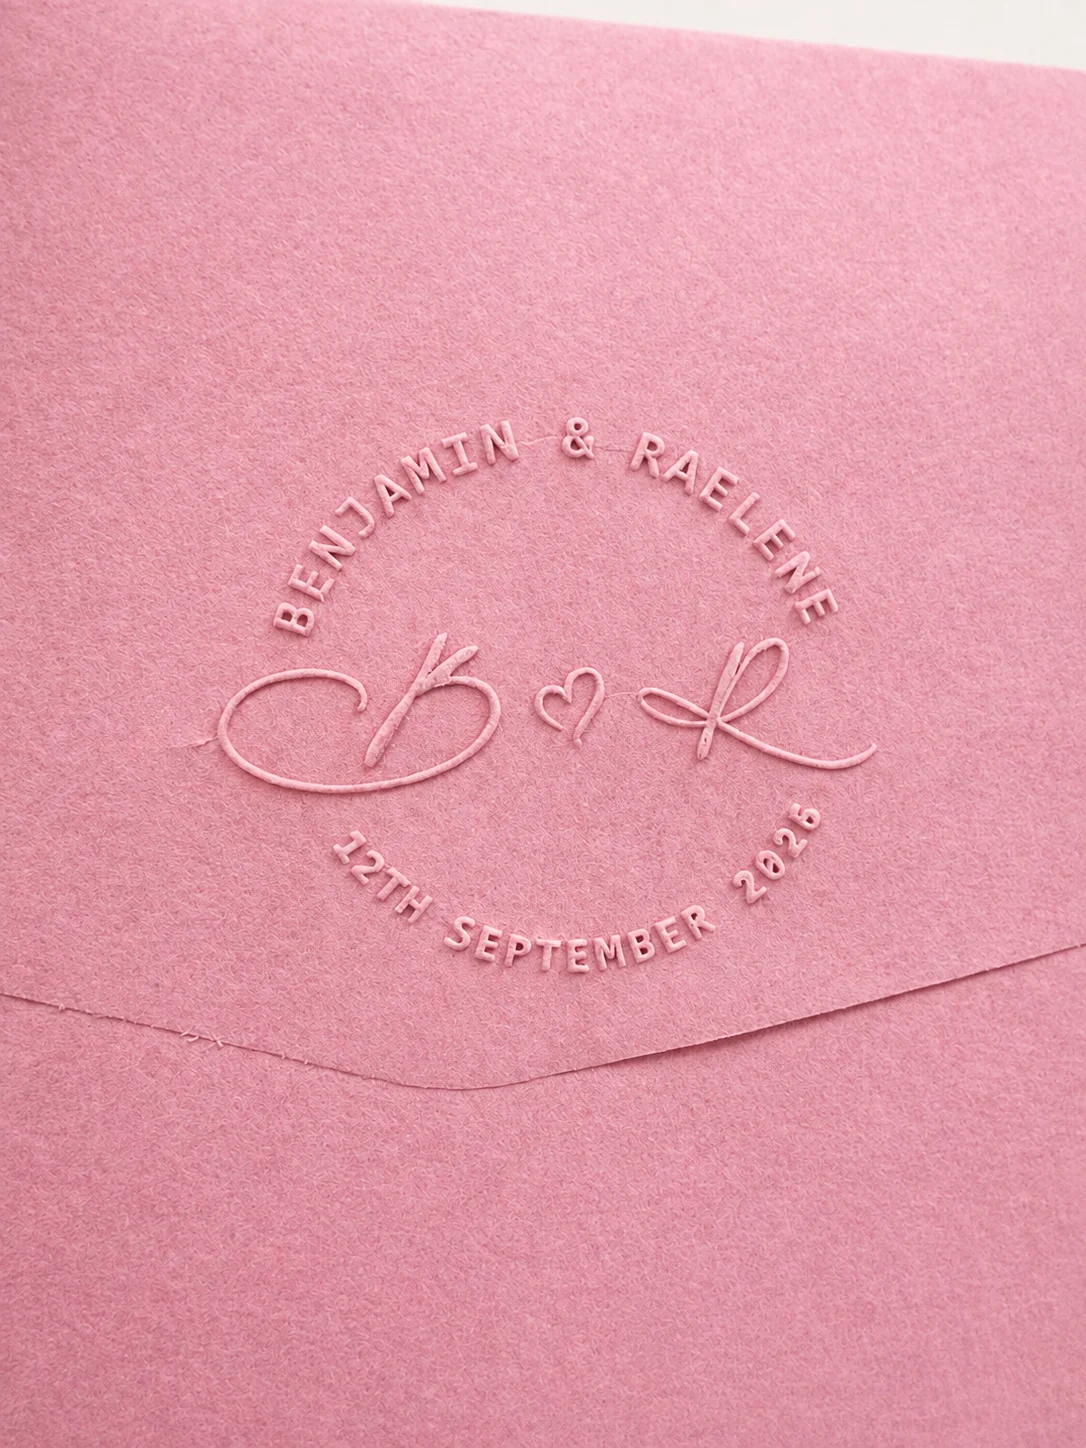
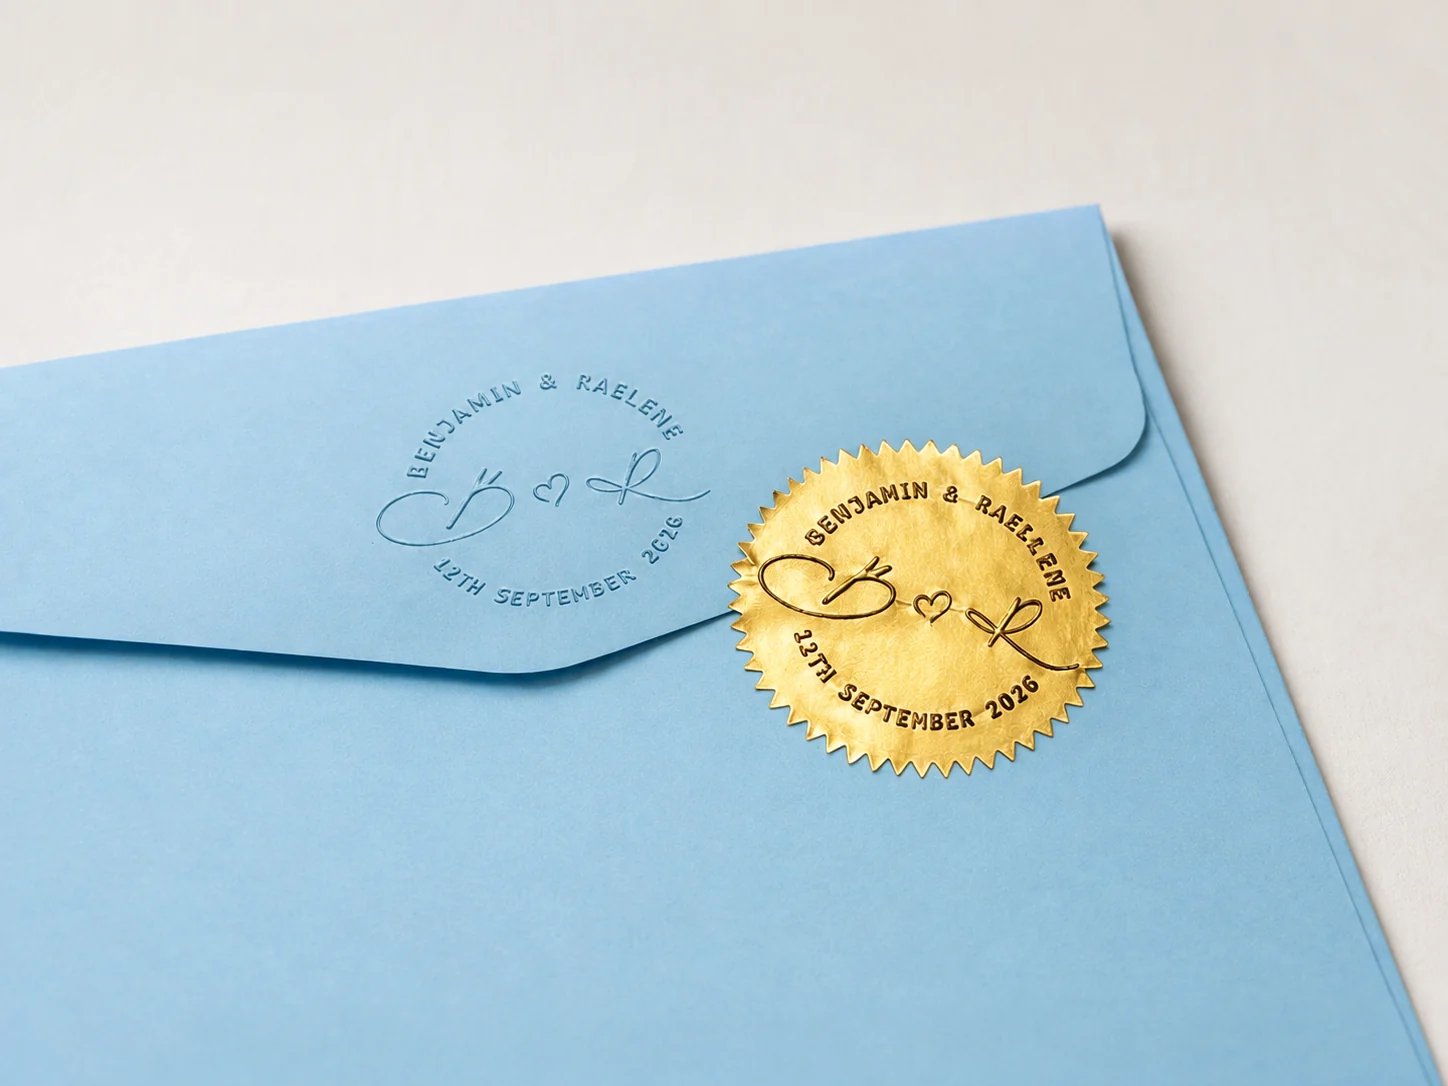
Embossing Verification on Real Materials
These photographs show additional real XLH Laser embossing examples on different target materials. They provide broader application evidence but are not presented as the same specimen used in the timed production test.
EVIDENCE DISCLOSURE
Production Test vs. Application Verification
The evidence on this page is intentionally separated so the documented timing and the broader application examples are not confused.
One Timed Male/Female Production Example
The laser video documents one real production example. Its independent timer provides the timing evidence for the matched POM die set shown in that test.
Additional Real XLH Application Examples
The assembly video and additional embossing photographs show the broader workflow and other real XLH Laser examples. They are not claimed to be the same timed specimen.
INTERPRETATION
Test Scope & Limitations
XLH-TEST-001 is a documented production example, not a universal specification for every artwork, machine setup or finished application.
The report does not establish that every artwork will be completed in 3 minutes 35 seconds.
It does not define a guaranteed hourly output because job preparation and production requirements vary.
It does not establish one die lifetime for all designs, hardware or target materials.
The shown examples do not prove compatibility with every paper, label, card or other substrate.
The report does not define one minimum line width or font size suitable for every die format.
Different artwork and production requirements should not be assumed to use identical processing settings.
TEST CONCLUSION
What XLH-TEST-001 Demonstrates
This report documents a complete production pathway from 1.7 mm POM laser processing on the DF60D 60W CO₂ laser to matched male and female die production, together with separate assembly and physical embossing verification.
The timed production example supports an approximately 3 minute 35 second laser-processing time for the specific die set shown. The separate assembly and application examples demonstrate how the broader POM embosser die workflow continues beyond the laser stage.
RELATED PRODUCTION RESOURCES
Explore the Connected XLH Laser Workflow
The test report is one evidence layer within a wider equipment, material, design and application system.
PRODUCTION DISCUSSION
Need to Validate Your Own Embosser Die Workflow?
Tell XLH Laser about your intended artwork, die format, material, embosser configuration and target substrate. We can discuss how the DF60D, POM die material and the surrounding production workflow fit together for your application.